

0102030405
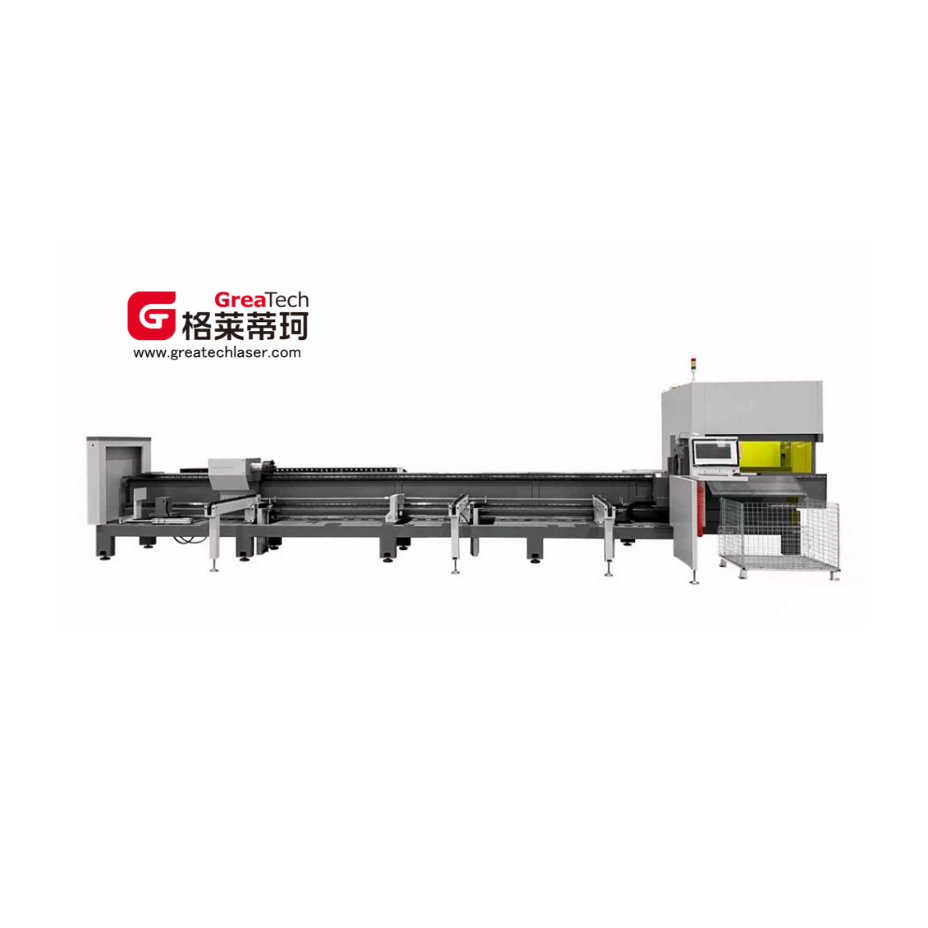
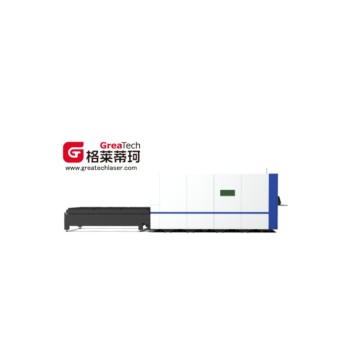
High-Speed Laser Pipe Cutting Machine G17-7017A from China Suppliers - Factory Direct with Material Saving Features
Key Component Configuration
| Order No. | Component Name | Brand | Model / Origin |
| Key Components | |||
| 1 | Fibre Laser | Ricke | 3000W – a top-tier domestic brand |
| 2 | Cutting Head | BOCI | 3000W – a top-tier domestic brand |
| 3 | Gear Rack | Specialty: Taiwan | M2-6 class / Taiwan, China |
| 4 | Reduction Box | TECHMECH / Modori | 090 / Germany |
| 5 | Linear Guide Rail | DTX / SMG | CGH30 / Taiwan, China |
| 6 | Motor | HuiChuan / HoChuan | High-performance motor, max speed 4000 rpm, bus-type configuration |
| 8 | Water Cooling Unit | Hanli / Teyu | Top-tier domestic brands |
| 10 | Electronic Control Element | Schneider, France | China |
| 11 | Airway Component | AIRTAC, Taiwan | China |
| Processing Components | |||
| 11 | Main Bed Frame | Self-developed, Suzhou | 9 meters / annealing at 600°C |
| 12 | Chucks (optional for 0 tailstock) | Self-developed, Suzhou | DRK-170 pneumatic / continuous air supply clamp |
| 13 | Auxiliary Feeding, Servo Floating Support Frame | Self-developed, Suzhou | 3 stents / 150 kg load capacity |
| 15 | Material Feeding Device, Feeding Frame (optional) | Self-developed, Suzhou | 20 kg per meter, max cutting length 2.0 meters |
| Software System | |||
| 15 | Operating System | Shanghai Baichu | Bus System / Shanghai |
| 16 | Material Matching Software | Shanghai Baichu | 3D Tube Cutting Software / Shanghai |
| Other | |||
| 17 | Operation Direction | Left-hand car | Standard configuration |
| 18 | Packaging and Transportation | Standard packaging | Standard configuration |
⚠️ Note: The industrial machine operates at 380±5V. Customers should install a voltage stabilizer based on actual conditions.
Component Technical Parameters
| Component Name | Attribute | Parameter Values |
| Laser | Output Power | 3000W |
| Work Pattern | Fiber Continuous | |
| Fibre Diameter | 50 μm | |
| Cooling Method | Hydrocooling | |
| Cuttable Material | Carbon steel, stainless steel, aluminum alloy, copper, brass, and other metals | |
| Lathe Bed | Structure | Tube sheet welding |
| Length | 8.5 meters | |
| Cartridge | Chuck Model | RDK160 |
| Work Pattern | Pneumatic | |
| Bearing | 150 kG | |
| Cutting Head | Focal Length | 125 mm |
| Collinear Focal Length | 100 mm | |
| Focal Speed | 100 mm/s (manual focus not available) | |
| Auxiliary Air Pressure | ≤3 MPa | |
| Water Cooling Unit | Cooling Medium | Distilled water / Deionized water |
| Ambient / Frozen Water Settings | 30 / 20 (adjustable) | |
| Temperature Regulation Accuracy | ±0.1 ºC | |
| Pump Capacity | 10 L/Min | |
| Pump Lift | 20 m |
Complete Machine Technical Parameters
| Class | Attribute | Parameter Values |
| Environment Attribute | Device Series | Small platform: 125 series |
| External Dimensions (mm) | 9600 × 3300 × 2300 | |
| Total Weight (tons) | About 3.5T | |
| Full Power Consumption (KW) | 20 ~ 25 | |
| Running Temperature (℃) | 0 – 40 | |
| Range of Work | Processing Path (mm) | Pipe diameter: 10–120 |
| Incision Width (mm) | 0.1–0.2 | |
| Y/X/Z/U Axis Stroke (mm) | 7000 / 150 / 250 / Unlimited rotation | |
| Resetting Accuracy / Speed | X/Y Axis Positioning Accuracy (mm) | ±0.03\1000 (7000±0.06) |
| X/Y Axis Repeatability (mm) | ±0.03 | |
| Cutting Accuracy | ±0.1 | |
| X-axis Rotation Repeatability (arc minutes) | ≤5 | |
| Maximum Rotation Speed of X-axis (RPM) | 130 HuiChuan | |
| Velocity and Acceleration | Maximum Acceleration of X/Y Axis | 1.5G |
| Maximum Idle Speed on X-axis (m/min) | 100 | |
| Maximum Idle Speed of Y-axis (m/min) | 130 HuiChuan | |
| Feed Parameters | Manual Feeding (mm) | 3000–6800 |
| Automatic Feeding Length (mm) | 5800 ~ 6200 | |
| Cycling Feed Cycle (s) | Initial loading ≤50, subsequent loading ≤20 | |
| Loading Machine Capacity (kg) | Semi-automatic: 200; Fully automatic: 1500 | |
| Max Load Capacity for Single Pipe – Manual Feeding (kg) | 150 | |
| Max Load Capacity for Single Pipe – Automatic Feeding (kg) | 150 | |
| Cutting Parameters | Tail Length (mm) | ≥45 mm |
| Minimum Cutting Length (mm) | Standard 2000 |
* The above technical specifications were established through testing on March 1, 2025.
Key Components and Motion Control
1. Bed Frame
Manufactured by welding sheet metal and tubing, the machine undergoes high-temperature annealing at 600°C, followed by 4.5 hours of heat preservation. After being slowly cooled to 200–300°C in the furnace, it is air-cooled to eliminate internal bed stress. The process includes rough machining followed by precision finishing, significantly enhancing the rigidity and stability of the machine tool while ensuring long-term stable accuracy. Featuring a side-mounted structure with an integrated automatic feeding system, this design effectively improves feeding efficiency and simplifies material handling.
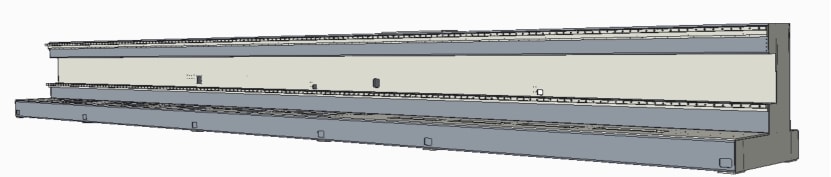
1.1 Rigidness: The bed structure is welded with plates and pipes, and reinforced with multiple ribbed tube plates to ensure transverse and longitudinal rigidity.
1.2 Welding: The welds on both sides are evenly distributed, symmetrically and staggered, to minimize welding deformation.
Annealing Report: Each bed number has an annealing report.
2. Crossbeam and X-axis / Z-axis Devices
2.1 The crossbeam undergoes annealing treatment to relieve internal stresses, ensuring the rigidity and stability of the laser head's moving components. During operation, limit switches control the travel distance for positioning, while elastic buffer pads at both ends provide mechanical limits to guarantee system safety.
2.2 The Z-axis mechanism primarily enables vertical movement of the laser head. This motion is controlled by the CNC system through servo motors, which drive linear actuators to move the Z-axis slider up and down reciprocally. Both ends utilize proximity switches to limit travel distance, ensuring safe and reliable operation.
3. Cutting Head and Following Part
3.1 Real-time monitoring of the sealed condition in the protected zone effectively extends the service life of the protective mirror and ensures stable production.
3.2 The impact-resistant cutting head design significantly reduces return-to-factory rates, eliminating the need for on-site service visits. Customers can perform replacements independently, resulting in lower maintenance costs.
3.3 A dust cover plate is added to the optical lens area to enhance the sealing grade of the core chamber and prolong the service life of the core lens.
3.4 The system is equipped with a high-precision capacitive sensing automatic tracking system, which enables highly stable Z-axis floating under system control, preventing height errors caused by thermal stress deformation or pipe surface irregularities during cutting.
4. Cooling System
The system employs Hanli, a renowned domestic brand, for its professional laser water chillers, which offer excellent stability and high precision. It features dual-channel temperature control, enabling independent temperature regulation for both the laser and cutting head, thereby ensuring more effective stability of the laser and cutting head. The functions include: water pressure alarm, high/low temperature alarm, voltage alarm, and various fault alarms.
Specific Parameters of Laser Special Cooling System
| Double Temperature and Double Control Laser Special Chiller | |
| Power Input | 220V / 50HZ |
| Cooling Medium | Distilled water / Deionized water |
| Water Temperature Control Accuracy | ±0.1 ºC |
| Set to Room Temperature Water | Standard 30°C (adjustable) |
5. Electrical Control System (Bachu Bus)
The electrical control system of the optical fiber tube cutting machine consists of three core components: the Bachu CNC system, servo system, and low-voltage electrical system. The system features a high-performance Bachu CNC system, a Windows-based PC-based CNC platform renowned for its rapid interpolation calculations and intuitive operation. The servo system incorporates imported AC servo motors and drivers, delivering stable performance, dynamic responsiveness, and high load capacity with user-friendly controls. The machine's soft keys enable customized functions across multiple operation modes, reducing physical buttons and simplifying the control panel. All operational functions are displayed via a menu interface, ensuring intuitive operation.
5.1 CNC System
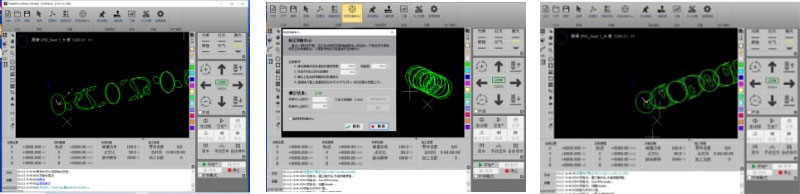
5.2 Advantages of CNC System:
1) The system features real-time bus-based control and adaptive cutting parameters, delivering twice the industry standard efficiency in corner cutting with stable corner-following and reliable cutting quality. It supports partial graphic processing, positioning at any point during stop/pause operations, and starting from any position. Additional features include fixed-height cutting, automatic edge detection, off-board tool engagement, and tool lifting.
2) It supports the separate setting of laser power, frequency, laser form, gas type, gas pressure, and follow-up height for the perforation process and cutting process.
3) Supports segmented perforation, progressive perforation, and pre-perforation. It allows setting separate parameters for the perforation process and cutting process, including laser power, frequency, laser type, gas type, gas pressure, and follow-up height.
4) Flexible and versatile automatic and manual sorting features, supporting partially fixed processing sequences by group. The unique sequence browsing function provides a more interactive view of processing sequences than simulation.
5) Set up the lead wire and cut seam compensation in the way of what you see is what you get. Automatically distinguish the inner and outer mold, and determine the cut seam compensation direction according to the inner and outer mold, and check the lead wire.
6) Unique one-touch calibration for horizontal square pipes, with automatic rotation center positioning.
5.3 Other Functions of the CNC System
- Surface height tracking control of pipe (following function)
- Undo
- Breakpoint return function
- Find Edge
- Suture compensation function
- Pulse cutting control function
- Frog jump function
- Import multiple parts
- Layout
- Quick conversion and batch processing
- Efficient automatic formatting
- The corresponding process database can be configured according to different materials and thicknesses
- Outline detection and graphic optimization processing
- Auto-optimize cutting path
- Perfect expert craftsmanship with flexible manual process adjustment
- Supports labeling and small hole marking
- Microconnect
- Weld compensation
5.4 Multiple Alarm Functions
The NC system of the machine has the function of self-checking and alarm and automatic protection, and the external condition has the function of alarm display and automatic protection.
6. Low-Voltage Electrical System
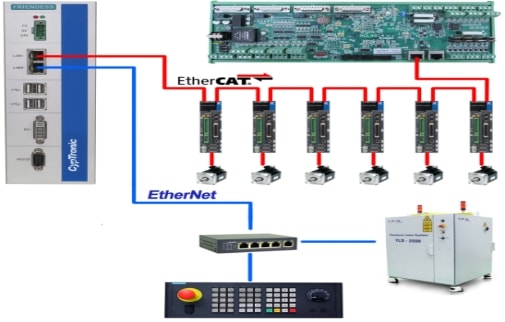
The low-voltage electrical system is located inside the electrical control cabinet, serving as the interface for the entire electrical control system. All components required for the electrical control system, including power supplies, relays, circuit breakers, contactors, and servo drive systems, are installed within the electrical control cabinet. The motor used is a bus motor, which reduces the number of wiring lines.
Connection diagram
Water, Electricity and Gas Demand
Electricity Demand
| Electricity Demand | Related Data | Notes |
| Three-phase five-wire 380~400VAC/50Hz distribution box | 380V±2% / 50Hz |
1. If voltage fluctuation exceeds 5%, a voltage stabilizer should be installed. A three-phase five-wire power supply of at least 45KVA is recommended. 2. The three-phase power supply must maintain an imbalance below 2.5% (Note: The 400VAC/50Hz/380V±2%/50Hz voltage must not experience sudden surges or power outages, as these may damage the laser). 3. The diameter of a single cable wire shall not be less than 10 square. 4. The power supply must be effectively grounded with a resistance ≤3Ω. 5. Three circuit breaker interfaces are required for the cutting machine wiring. |
Cooling Water Requirement
| Cooling Water Requirement | Related Data | Notes |
| Chiller Water | Distilled water / Deionized water | 30L, conductivity less than 10 μS |
Protective Gas Demand
| Protective Gas | Related Data | Notes |
| Oxygen | Purity: ≥99.6% Gases with purity below 99.6% may affect cutting performance and quality. |
Cutting carbon steel and various iron plates with oxygen-assisted cutting achieves high-quality and efficient results. |
| Pressure: 1 MPa Flow rate ≥ 1 m³/min |
||
| Nitrogen | Purity: ≥99.99% Gases with purity below 99.99% may adversely affect cutting performance and quality. |
Cutting of stainless steel and galvanized sheets is performed with nitrogen-assisted cutting, achieving high-quality results. |
| Pressure: 2.5 MPa Flow rate: ≥2.5 m³/min |
||
|
1. Bottled gas requires the installation of a pressure reducing valve for the cylinder. 2. Oxygen (O₂) pressure reducing valve: The adjustable outlet pressure range is 0.4 MPa to 1.2 MPa, with a pressure fluctuation range of 1%. 3. Nitrogen (N₂) pressure reducing valve: The adjustable outlet pressure range is 0.4 MPa to 5 MPa, with a pressure fluctuation range of 1%. |
||
| Air | Working pressure ≥1.3 MPa |
1. If air cutting is required, the user shall provide a compressor, refrigerated dryer, air receiver, and four-stage filtration (filtering precision 0.01 microns). 2. The gas in the air-to-laser cutting machine must be free of water and oil, as these contaminants may compromise cutting quality and reduce the lifespan of various lenses. 3. The condensation point temperature must not exceed 5°C. 4. Oil content ≤0.003 ppm, solid particles ≤0.01 μm |
| Flow rate ≥ 1.8 m³/min | ||
Frequently Asked Questions (FAQ)
Q
What laser power does this fiber laser tube cutting machine use, and what materials can it cut?
This machine is equipped with a 3000W fiber laser (Ricke brand). It is capable of cutting a wide range of metals including carbon steel, stainless steel, aluminum alloy, copper, brass, and other metallic materials with high precision and efficiency.
Q
What are the pipe diameter and cutting length specifications of this machine?
The machine supports a pipe diameter range of 10–120 mm. The Y-axis stroke is 7000 mm. Automatic feeding length is 5800–6200 mm, and manual feeding length is 3000–6800 mm. The minimum cutting length is 2000 mm (standard), with a tail length of ≥45 mm.
Q
What type of power supply is required for installation, and are there specific electrical requirements?
The machine requires a three-phase five-wire 380V±2% / 50Hz power supply with a minimum capacity of 45KVA. The power supply must be effectively grounded (resistance ≤3Ω), and voltage fluctuation must not exceed 5%. If fluctuation exceeds this limit, a voltage stabilizer must be installed. Three circuit breaker interfaces are required for wiring.
Q
What gases are required for operation, and what purity levels are needed?
The machine uses three types of gases: Oxygen (purity ≥99.6%, pressure 1 MPa) for cutting carbon steel and iron plates; Nitrogen (purity ≥99.99%, pressure 2.5 MPa) for cutting stainless steel and galvanized sheets; and Air (working pressure ≥1.3 MPa) for general air-assisted cutting. All gases must be free of water and oil contamination to protect the optical lenses.
Q
What CNC control system does this machine use, and what are its key software features?
The machine uses the Shanghai Baichu Bus CNC system — a Windows-based PC platform featuring real-time bus control, adaptive cutting parameters, and 3D tube cutting software. Key features include automatic edge detection, breakpoint return, frog jump function, suture compensation, auto-optimize cutting path, segmented/progressive perforation, and a comprehensive process database configurable by material and thickness.
Q
How is the bed frame constructed, and what makes it durable for long-term use?
The bed frame is manufactured by welding steel plates and tubing, then subjected to high-temperature annealing at 600°C with 4.5 hours of heat preservation, followed by slow furnace cooling to 200–300°C and air cooling to eliminate internal stress. This process, combined with rough and precision machining, ensures exceptional rigidity, stability, and long-term accuracy. The 9-meter bed is self-developed in Suzhou and comes with an individual annealing report for quality traceability.