

01
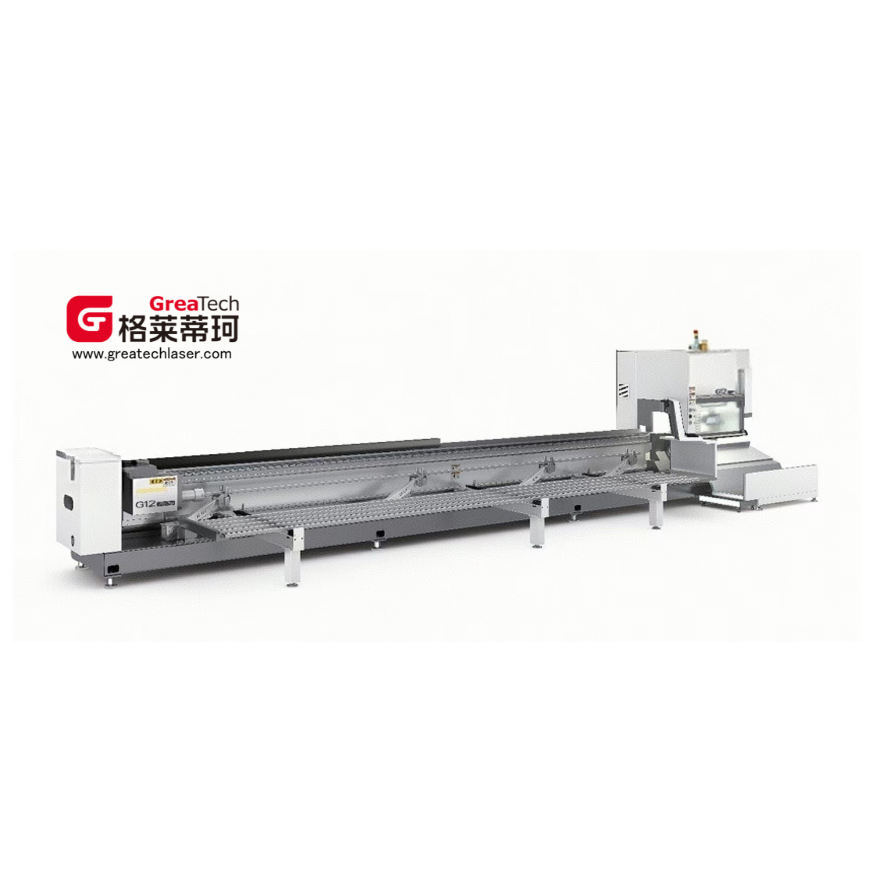
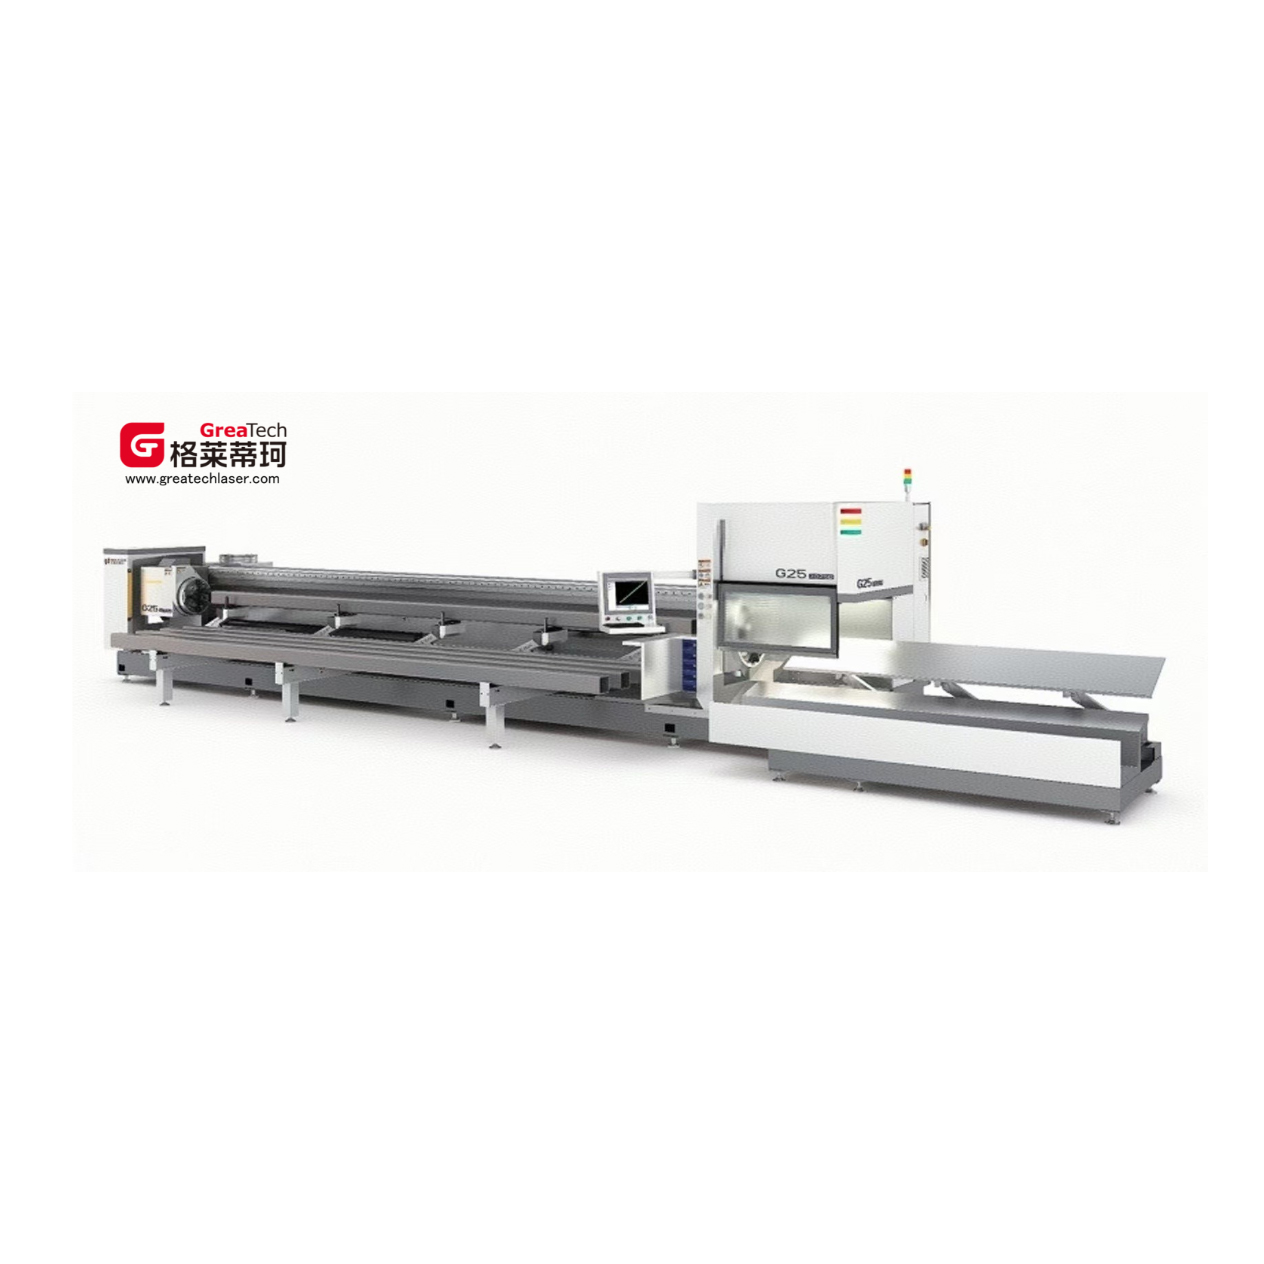
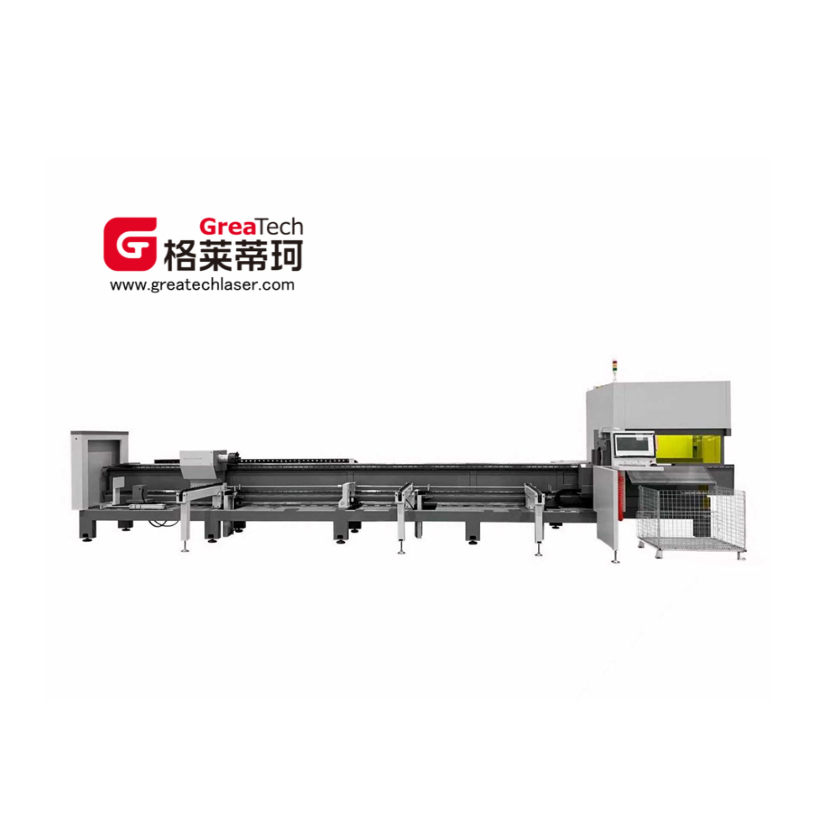
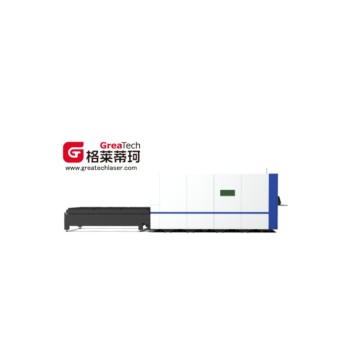
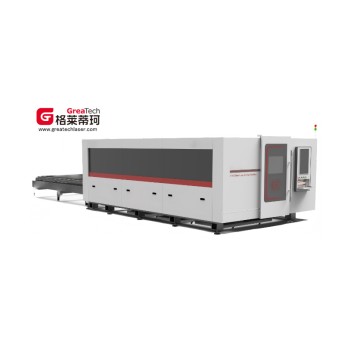
Laser Pipe Cutting Machine G17-7017A (Two-Chuck)
Application
The bed: It is made of plates and pipes through welding. After annealing at a high temperature of 600 degrees, it is kept warm for 4.5 hours, then slowly cooled in the furnace to 200-300 degrees before being taken out of the furnace for air cooling. This process eliminates the internal stress of the bed. After rough machining, finish machining is carried out, which greatly improves the rigidity and stability of the machine tool and ensures its long-term stable precision. The side-hanging machine tool structure, equipped with an automatic feeding machine, can effectively improve the feeding efficiency and simplify the blanking process.
Rigidity: Welded with plates and pipes, the bed structure is connected with the horizontal and vertical beds by multiple reinforcing rib tube plates to ensure rigidity.
Welding: The welds on both sides are evenly distributed, and symmetric and staggered welding is adopted to reduce welding deformation.
Annealing report: Each bed number is accompanied by an annealing report.
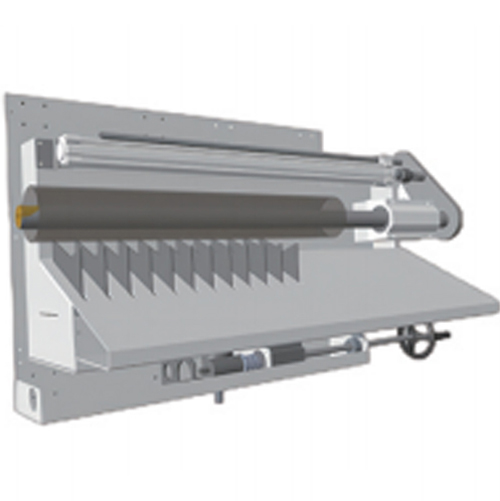
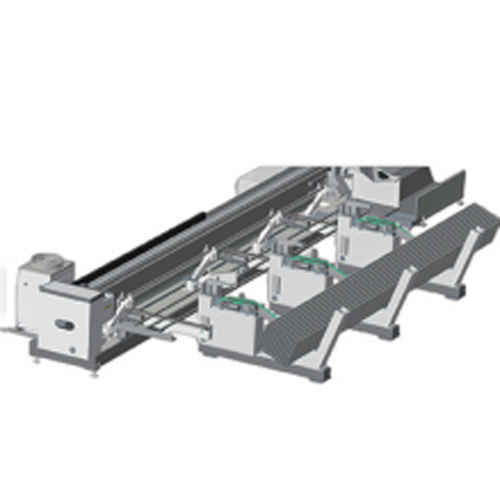
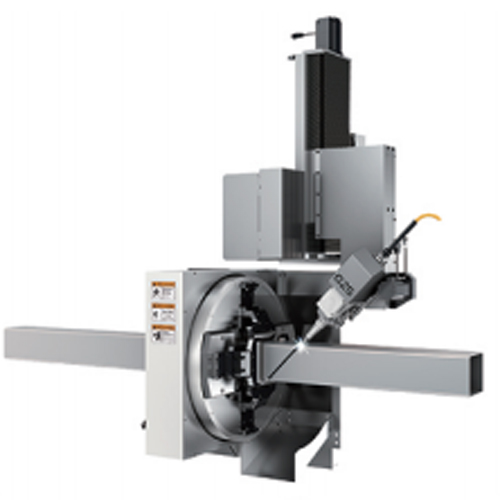
Beam and X-axis, Z-axis devices
The beam is annealed to eliminate internal stress, ensuring the rigidity and stability of the laser head's moving components. During movement, the limit switch controls the stroke for limiting, and there are also elastic buffer pads at both ends for mechanical limiting to ensure the safety of the system operation.
The Z-axis device mainly realizes the up and down movement of the laser head. The up and down movement of the laser head is controlled by the numerical control system through the servo motor, which drives the linear module to drive the Z-axis slide plate to reciprocate up and down. Proximity switches are used at both upper and lower ends to control the stroke, ensuring the safety and reliability of the movement.
Cutting head and follow-up parts
The tightness of the protection area under real-time monitoring effectively prolongs the service life of the protective mirror and ensures stable production.
The anti-collision design of the cutting head effectively reduces the probability of returning to the factory. There is no need for after-sales staff to come to the door, and customers can replace it by themselves, resulting in lower maintenance costs.
A dust-proof cover plate is added to the optical lens area to improve the sealing level of the core chamber and extend the service life of the core lens.
Equipped with a high-precision capacitive sensing automatic tracking system, under the control of the system, it can realize a very stable Z-axis floating function, preventing height errors caused by thermal stress deformation or uneven pipes during pipe cutting and processing;